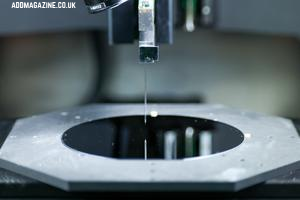
On a large OLED panel, a single broken data line shows up as a thin vertical stripe running the full height of the screen. Inspection usually catches it at the array stage, long before anyone sees it on a showroom wall, and at that point the break might be only a few microns across. The engineer looking at it has to decide whether the panel gets repaired or scrapped, and when the glass it sits on carries several panels at once, that decision has real money attached.
Semiconductor packaging lines deal with their own version of the same problem. As chips get split into chiplets and placed side by side on interposers or stacked on top of each other, the wiring between them keeps shrinking, and a defect measured in microns can ruin a package worth far more than the materials in it. In both industries the margin for error has narrowed faster than many of the tools used to put material down.
The growing demand for greater accuracy in modern production processes
Most of the pressure comes from density. Displays keep adding pixels, particularly in phones, watches and the micro-displays inside AR and VR headsets, where pixel pitch is measured in single-digit microns. Packages carry more input and output connections in less area, with redistribution layers and bump pitches that would have looked unrealistic for packaging ten years ago.
Conventional patterning handles a lot of this well, but it was designed to do the same thing millions of times across a whole wafer or panel. It’s much less suited to putting a small amount of material in exactly one spot, and that’s what repair, prototyping and several of the newer packaging steps actually call for. This is where advanced precision deposition technology has started to earn attention, because it lets engineers place conductive inks, dielectrics and other functional materials directly where they’re needed, in a single step, without coating an entire surface and then etching most of it away again.
Accuracy in this context means several things at once. Line width is the obvious one, yet placement accuracy matters just as much, and so does consistency, meaning whether the hundredth line looks like the first, whether the edges are clean and whether stray droplets land somewhere they could cause a short. A process that can draw a 2 µm line but scatters satellite drops around it isn’t much help next to a dense array of thin-film transistors.
Where conventional methods start to struggle
Photolithography is still the workhorse of front-end semiconductor fabrication, and nothing described here replaces it there. It does depend on masks, resist coating, exposure, development and etching, though, and every one of those steps adds time and cost. For a single repair, a short prototype run or a change to one layer of a design, that whole sequence is hard to justify.
Inkjet printing took over part of that ground because it’s additive and maskless, and it’s already used in production for certain display layers. Its limits show up at fine scales. Droplets are usually measured in picoliters, which keeps printed features in the tens of microns on most systems, while satellite drops, coffee-ring edges and spreading on low-energy surfaces all eat into precision. Aerosol jet and electrohydrodynamic printing push resolution further, each with its own trade-offs around overspray, substrate charging or a narrow process window.
| Method | Typical feature scale | Strength | Limitation |
| Photolithography and etch | Down to nanometers | Mature and wafer-scale | Masks, many steps, subtractive |
| Inkjet printing | Tens of microns | Maskless, quick over large areas | Satellite drops, edge spreading |
| Aerosol jet | Around 10 µm | Prints on curved parts | Overspray at the edges |
| Electrohydrodynamic jet | Sub-micron to a few microns | High resolution | Sensitive to substrate and charging |
| Capillary micropen printing | About 50 µm down to a few hundred nm | Single step, follows topography | Serial, suited to targeted work |
Ranges are typical and vary with the system, the ink and the substrate.
How improved material control leads to better yields and new design possibilities
Yield is usually where the business case gets made. If an open line on a display backplane can be bridged with a few microns of conductive ink in precisely the right place, the panel carries on down the line instead of being downgraded or thrown out. Display makers have been repairing defects for years, often with laser-based methods, and finer additive deposition widens both the range of defects that can be fixed and the materials available to fix them.
The same logic holds further upstream. When a process controls the volume and position of every deposit closely, you get fewer shorts from stray material, fewer opens from thin or broken lines and less variation from one part to the next, and each of those shows up directly in yield figures. Less waste is a side benefit, which matters when the ink is loaded with silver or another costly metal and most of it would otherwise be etched off and discarded.
Tighter control also changes what designers are prepared to try. Printing that adapts to surface topography can run a conductive track over a step, down the side of a die or across a substrate that isn’t flat, opening up interconnect routes that are awkward or impossible with processes built for flat wafers. Teams working on micro-LEDs, sensors, photonic components and flexible circuits can often test a new layout within a day or two, without waiting weeks for a fresh mask set.
For research groups and pilot lines, that speed is frequently the bigger advantage. Being able to iterate on micro-scale electronics manufacturing directly, without needing a full fab behind every experiment, shortens the distance between an idea on a whiteboard and a working sample on the probe station.
Why the ink matters as much as the machine
Precision isn’t only a property of the hardware. An ink’s viscosity, particle size, solvent and surface tension decide how a line spreads once it touches the substrate, how it dries and whether it stays where it was put. Nanoparticle silver inks are a good example, since the particles need to be far smaller than the line they’re meant to form, or the edges turn ragged and the narrowest sections can clog or break.
Substrate preparation plays its part as well. A surface that’s slightly too wettable lets a line spread wider than planned, while one that repels the ink can make it bead up into a row of dots. Cleaning, plasma treatment and humidity control all affect the result, and their influence grows as features get smaller, which is why engineers working at the micron scale spend a surprising share of their time on chemistry rather than mechanics.
Systems that accept a wide range of viscosities give engineers more freedom on this front. They can choose a material for its electrical, optical or biological properties first and worry less about whether the printer can handle it, which matters a great deal when the goal is a working sensor or a conductive bridge and not simply a neat line on a test coupon.
Where precision deposition fits on the factory floor
None of this means additive printing replaces the existing toolset. In most fabs it sits alongside it and takes on the jobs that conventional processes handle poorly. Because tip-based and jet-based methods deposit material serially, they’re better matched to targeted, high-value work than to coating whole panels, and the most common uses reflect that.
- Open-line and short repair on display backplanes.
- Interconnect rework in advanced packaging.
- Prototype circuits and test structures.
- Electrodes for biosensors.
- Conductive tracks over uneven or 3D surfaces.
- Functional layers in photonics research.
What to look for when evaluating a deposition process
Anyone comparing systems for fine-feature deposition tends to end up asking the same handful of questions, and it helps to have them written down before the first vendor demo.
- Minimum line width, and the spacing you can hold between lines.
- Placement accuracy relative to existing features.
- Range of inks, viscosities and substrates.
- Whether satellite drops or overspray appear at the edges.
- How the system copes with steps and uneven topography.
- Throughput for the job you actually need to run.
- Post-processing, such as curing or sintering temperatures.
That last point deserves more thought than it usually gets. Many conductive inks need heat to reach useful conductivity, and the temperature has to suit everything else already on the substrate. A polymer film or a finished package can’t be treated the way a bare silicon wafer can, so an ink that sinters at a lower temperature can matter more than a slightly finer line.
It’s also worth testing on your own parts rather than on the vendor’s sample coupons. A process that prints beautifully on clean glass can behave quite differently on a populated board with mixed surface energies, and a short trial on real material usually answers more questions than a spec sheet.
Looking ahead
Display roadmaps built around micro-LED and high-density micro-OLED, together with the semiconductor industry’s move toward chiplets and heterogeneous integration, all lead in the same direction: smaller amounts of material, placed in more precise locations, on more varied surfaces. Ultra-accurate deposition used to be a laboratory curiosity, but it’s increasingly a practical tool on pilot lines and in repair cells.
Manufacturers who can deposit material with that level of control get more usable product out of every substrate they process, and more room to try designs that older methods would have ruled out early. For an industry where a few microns can decide whether a part ships, that combination is hard to ignore.